Hey everyone, it’s Jake here—been selling iron cores for just over 8 years now, and let me tell you, one question I get asked nonstop is: "How do I make my iron core perform better?" Whether you’re winding transformers, inductors, or even electric motor parts, a dud iron core can tank your whole project, no matter how good the rest of the parts are. I’ve seen it all: guys throwing a cheap core in and wondering why their unit’s overheating, or wasting money on premium stock that’s not actually optimized for their specific use. Today, I’m breaking down real, actionable stuff—no fancy textbook jargon, just what I’ve tested in my warehouse and what our regular customers swear by. Iron Core
First off, let’s get one thing straight: "performance" for an iron core isn’t one-size-fits-all. If you’re making a small signal inductor for a phone charger, your needs are totally different from a big transformer for a factory motor. That means the first step to optimizing your core is actually figuring out what your core needs to do. I once had a customer, a small electronics repair guy, order a high-grade silicon steel core for a portable drill motor—turns out he just needed a lower-core-loss grade, and the extra material cost was making his repair prices uncompetitive. Don’t make that mistake: list out your operating frequency, voltage, power load, and temperature range first. That baseline keeps you from overspending or underperforming.
Now, let’s talk material choice—this is the bread and butter of my job, and it’s where 70% of performance optimizations start. Most people don’t realize iron cores aren’t just plain iron. The two big players are silicon steel (also called electrical steel) and pure iron (usually low-carbon or electrolytic iron). Silicon steel is the workhorse for high-frequency or high-power applications because it has way lower core loss—you know, that energy that gets wasted as heat when the core’s magnetic domains flip back and forth with the AC current. Add 3-5% silicon to iron, and you drop core loss by like 50% right off the bat. It also makes the core more brittle, but for most power stuff, that’s a tradeoff worth making.
Pure iron, on the other hand, has higher saturation flux density—that’s the maximum magnetic field the core can hold before it stops working effectively. If you’re making a small, high-power inductor for an electric car’s charging system, pure iron might be better because it can handle more power without saturating, so you don’t need a bigger, heavier core. We stock both, but I always tell customers: if your operating frequency is over 1kHz, go silicon steel. Under that, pure iron might be the cheaper, better bet. There’s also specialty stuff like amorphous metal cores for super-high-frequency applications—they have almost zero core loss, but they’re way more expensive, so only go for that if you’re dealing with 10kHz+ small signal stuff.
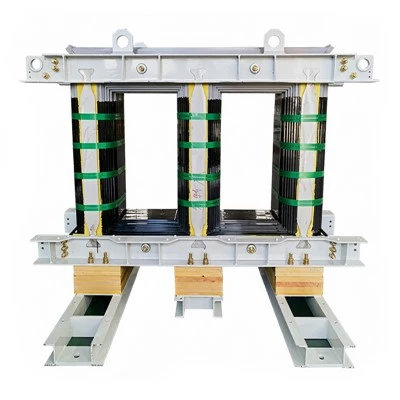
Next up, core construction, and this is where I see a lot of guys cutting corners that kill performance. Most iron cores are laminated, right? Thin sheets of metal stacked together instead of a solid block. Why? Because eddy current loss. A solid core is like a single big loop for electricity to flow, so when the magnetic field changes, it induces huge currents in the whole core, making it heat up like a toaster. Laminating the core—each sheet just 0.1 to 0.5 mm thick—breaks up those loops, cuts eddy current loss by a ton. But here’s the trick: the thinner the laminations, the lower the loss. That’s why high-frequency cores use 0.1mm thick sheets, while low-power stuff can get away with 0.5mm.
Wait, but it’s not just the sheets—how you stack them matters too. We recommend interleaving laminations if you’re dealing with high voltage. If you stack all the positive-sided sheets on top and negative on the bottom, you get bigger voltage differences between adjacent sheets, which can lead to arcing between layers. Interleaving alternates positive and negative, keeps the voltage between sheets low, and boosts insulation too. Also, make sure the laminations are properly insulated from each other—even a tiny scratch on the coating can create a path for eddy currents, turning your optimized laminated core into a hot mess. We apply a thin organic insulation coating to all our silicon steel laminations for exactly this reason, and it’s worth the extra cost.
Then there’s air gaps, and this is the trickiest part to get right, but it can make or filter core performance, especially for inductors. When you need an inductor that doesn’t saturate even at high current, you add a small air gap to the core. The air gap increases the core’s effective reluctance, so it can handle more current before hitting saturation. But here’s the mistake people make: if you just cut a single gap in the core, you get fringing flux—magnetic lines that bend around the gap and leak out into the surrounding area. That fringing flux can hit the winding wires, cause extra losses, and even interfere with other components.
How do we fix that? We use multiple small air gaps instead of one big one. Split the core into two or three pieces, each with a tiny gap, so the fringing flux is spread out instead of concentrated in one spot. Also, use non-conductive gap material—like fiberglass or ceramic paper—instead of just leaving an air space. If you use metal shims, they’ll conduct the magnetic flux and cause extra losses. I’ve had a customer swap a single-gap core for a multi-gap one and see a 15% drop in temperature without changing the size or cost of the core—game changer.
Surface treatment and finishing are two more things people sleep on, and they can make a huge difference in performance and longevity. Corrosion is a big one—if your iron core rusts, the rust is non-magnetic, so it messes with the magnetic path and increases loss. We have three standard finishes: hot-dip galvanizing for outdoor or high-humidity applications, a phosphate coating for general use, and an epoxy powder coat for super tough environments like industrial equipment. But wait—don’t over-coat. If you put a thick finish on laminations, it takes up space between the sheets, so you have to stack fewer laminations to get the same core size. That leads to lower saturation and higher loss. We keep our finishes thin—10 to 20 microns—so you get corrosion protection without losing core volume.
Another finishing tip: if you’re machining your core after you get it, make sure you deburr and re-insulate any scratched areas. Machining exposes the raw metal and scrapes off the insulation coating, so you’ll get eddy current loss where you didn’t expect. We offer post-machining touch-up coating as an add-on, and it’s one of our most popular little extras because it saves customers from performance headaches later.
Now, let’s talk about a common myth I hear all the time: "polishing the core surface makes it more efficient." No, not really—unless you have rough gaps. If you leave burrs on the gap area, they create an uneven gap, which concentrates the magnetic flux and increases fringing. But polishing the flat faces of laminations doesn’t do much for core loss. The biggest win here is just keeping the core free of debris—dust, oil, or metal shavings between laminations can act as conductors and create eddy current paths. When a customer gets their core from us, we always include a small microfiber cloth and a note to wipe it down before assembling, and I swear by that simple step.
Wait, one more big one: proper winding and assembly. Even the best core in the world is useless if you wind the wrong wire or assemble it wrong. When you wind coils around the core, make sure the winding is tight and evenly distributed. If the winding is lumpy or loose, the wires can move, cause friction, and even short out, leading to extra heat. Also, leave enough space between the winding and the core to add insulation, but not so much that air gaps are introduced accidentally. When assembling the core halves, use a non-magnetic fastener—like stainless steel or aluminum—instead of steel bolts. Steel bolts will act as a short circuit for magnetic flux, causing huge losses. We supply all our core customers with non-magnetic fasteners for exactly that reason, and it’s saved so many of them from testing failures.
Let me give you a real example to tie all this together. A few months back, a customer came to us with a 5kW transformer that was overheating 10 degrees higher than it should. He’d bought a cheap silicon steel core from another supplier, no proper insulation, a single air gap, and a thick galvanized finish that ate up core volume. We swapped him for our standard 0.2mm insulated laminations, used a multi-gap design, skipped the overdone galvanization for phosphate coating, and walked him through winding it tight with non-magnetic bolts. He tested it a week later—was running at the perfect temperature, and his energy efficiency went up 8%. That’s not a magic trick, that’s just applying all the stuff I’ve been talking about.
Before I wrap this up, let’s recap the key points so you don’t have to scroll back: 1) Know your use case first—frequency, power, environment, that’s your baseline. 2) Pick the right material: silicon steel for high-frequency/power, pure iron for high saturation, amorphous for super high-frequency small stuff. 3) Go thin laminations for high frequency, make sure they’re properly insulated. 4) Use multi small air gaps instead of one big one, with non-conductive gap material. 5) Finish smart—thin corrosion protection, don’t over-coat, touch up machining scratches. 6) Assemble right: non-magnetic fasteners, tight even windings, no debris gaps.
If you’re still figuring out what core is right for your project, or you’ve got an existing core that’s underperforming and you want to troubleshoot it, hit us up. We don’t just sell cores—we help guys like you optimize their designs, no fluff, no hidden fees. Just send over your specs, and we’ll hook you up with the right core for your needs.
Transformer Accessories References
- Electrical Steels for Rotating Machines, American Iron and Steel Institute, 2021.
- Magnetic Components Design Handbook, Wiley-IEEE Press, 2019.
- Core Loss Reduction in Laminated Iron Cores, Journal of Applied Magnetics, Vol. 22, No. 3, 2017.
- Air Gap Effects on Inductor Performance, Power Electronics Society Conference Proceedings, 2020.
Wuxi Zhongpu Electric Co., Ltd.
As one of the most professional iron core manufacturers and suppliers in China, we also support customized service. Please feel free to wholesale bulk high quality iron core made in China here from our factory. Welcome to contact us for pricelist.
Address: No.52 Jiankang Road, Donggang Town, Xishan District, Wuxi City, Jiangsu Province
E-mail: 13585006135@163.com
WebSite: https://www.zhongpuelectric.com/
